
 Send Inquiry
Cashew Metal Detector
Price 200000.00 INR/ Unit
MOQ : 1 Unit
Cashew Metal Detector Specification
- Rejecter
- Automatic pneumatic pusher rejection system
- Application
- Detection of ferrous and non-ferrous metal contaminants in cashew processing lines
- Function
- Automatic metal detection and rejection system for enhanced food safety
- Sensitivity
- 2 mm to 4 mm ferrous, 3 mm to 6 mm non-ferrous (customizable as per product)
- Power Supply
- 230V AC, 50Hz (standard), other voltages available on request
- Conveyor Speed
- Variable, up to 25 meters/minute
- Frame Construction
- Stainless steel 304 with mirror polish finish
- Finish
- Corrosion resistant and easy to clean for food environments
- Display Type
- Digital (LED/LCD) with sensitivity adjustment
- Detection Tunnel Size
- Customizable as per cashew product requirements
- Belt Type
- PU Food Grade Conveyor Belt
- Weight Capacity
- Up to 20 kg per batch (customizable)
- Operating Temperature
- 0C to 45C
- Alarm Indication
- Audio/Visual (buzzer and tower light)
- Control Panel
- Microcontroller based electronic display
Cashew Metal Detector Trade Information
- Minimum Order Quantity
- 1 Unit
- Supply Ability
- 30 Units Per Month
- Delivery Time
- 1 Months
Cashew Metal Detector About
The Cashew Metal Detector is a valuable piece of equipment that ensures the safety and quality of cashew products by detecting and removing any metal contaminants in the product. This Cashew Metal Detector is made of high-quality materials, ensuring durability and longevity, and has a compact design, making it easy to install and operate. It helps in increased efficiency, making it an essential tool for the food industry. Its properties include high sensitivity, reliable performance, and user-friendly interface, making it a valuable asset for any cashew processing facility.
Product details
|
Power Source |
Electric |
|
Frequency (Hz) |
50 Hz |
|
Brand |
Locus Exim |
|
Material |
Mild Steel, Stainless Steel |
|
Phase |
3 |
|
Surface Finishing |
Polished |
|
Voltage |
240 V |
Enhanced Food Safety in Cashew Processing
Equipped with sophisticated detection technology, this machine safeguards against ferrous and non-ferrous contaminants, playing a pivotal role in maintaining food safety standards. Its automatic rejection mechanism minimizes manual intervention, ensuring batch integrity and preventing metal-tainted products from reaching the market.
Robust and Hygienic Construction
The stainless steel 304 frame, mirror polish finish, and food-grade PU conveyor belt ensure durability and effortless cleaning. IP65 waterproofing further supports washable, moist environments, making the system suitable for continuous food processing operations where hygiene is paramount.
User-Friendly Operation with Custom Features
A digital LED or LCD display with sensitivity adjustment allows precise control over detection parameters. The variable conveyor speed, customizable tunnel sizes, and adaptable weight capacity mean this detector can be tailored for different cashew product lines and production scales, making it a versatile solution for diverse processing needs.
FAQs of Cashew Metal Detector:
Q: How does the Cashew Metal Detector improve food safety in processing lines?
A: The detector automatically scans and removes any ferrous or non-ferrous metal contaminants present in cashew products. Using a highly sensitive detection system and an automatic pneumatic rejection mechanism, it ensures only contaminant-free batches proceed, safeguarding consumer health and upholding regulatory standards.Q: What customization options are available for different cashew processing requirements?
A: The machine offers customizable detection tunnel sizes, sensitivity ranges, and weight capacities. This flexibility allows manufacturers to select the ideal settings based on their specific cashew products and desired throughput, ensuring precise and efficient operation.Q: When should regular maintenance be performed on this metal detector?
A: Routine maintenance is recommended based on usage frequency and working environment. Generally, regular cleaning of the belt and tunnel, along with periodic inspection of electronic and pneumatic components, keeps the system running efficiently and prolongs its lifespan.Q: Where is this metal detector best suited for installation?
A: Designed for food processing environments, the detectors corrosion-resistant, IP65-rated construction makes it ideal for cashew processing plants, especially where moisture and wash-down cleaning are common. Its adaptability also suits other nut and food production facilities.Q: What is the process for detecting and rejecting contaminated cashew batches?
A: As cashews pass along the food-grade conveyor, the detector scans for metal particles within the customizable sensitivity range. If contamination is detected, an audio/visual alarm activates, and the integrated pneumatic pusher automatically diverts the affected batch for removal, ensuring contamination-free output.Q: How easy is it to use and adjust the metal detector for different products?
A: The microcontroller-based control panel with digital LED or LCD display enables straightforward operation. Sensitivity settings and tunnel size are easily adjusted to match different product specifications, supporting versatile use across various cashew grades and batch sizes.Q: What are the primary benefits of using this system for cashew exporters, manufacturers, and suppliers?
A: Key advantages include assured product safety, compliance with export standards, reduced manual inspection, efficient processing, and robust performance even in demanding, hygienic environments. These contribute to enhanced brand reputation and reduced risk of product recalls.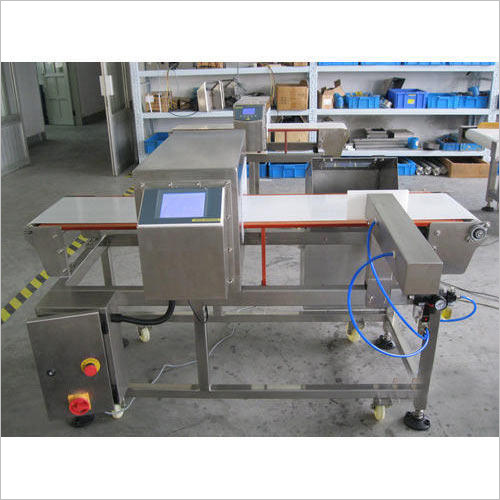
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email


LOCUS TECHNOLOGIES
GST : 27AAJFL9220A1ZK
Contact Details
- Ground Floor, Building No.Survey 96/2, Gatha Mandir, Bypass, Dehu Road,Pune - 412109, Maharashtra, India
- Phone : 08045476607
- Mr Vinay Pawar (Founder and CEO)
- Mobile : 08045476607
- Send Inquiry
- Branch Location: Shed No. B-1, Angol Industrial Estate,
Udyambaug [Belgaum] 590008
Pune Office Address: Gat No. 96, Survey No. 02, Vitthalwadi Bypass Road, Dehu(Vitthalwadi) , Pune: 412109 Maharashtra, India.
 Send Inquiry

|


 Send Inquiry
 Send SMS
 Call Me Free
LOCUS TECHNOLOGIES
All Rights Reserved.(Terms of Use)
Developed and Managed by Infocom Network Private Limited.
Developed and Managed by Infocom Network Private Limited.


